How to Choose a Copper Stamping Machine?
Choosing a Copper Stamping Machine requires more than comparing price, tonnage, and catalog photos. The right decision begins with the part itself. Copper thickness, alloy hardness, shape, and production volume all affect machine performance. A thin connector may need precise feeding, while a thick busbar demands greater forming force. Small details matter.
In practical factory evaluations, I examine stroke length, slide speed, die compatibility, and material feeding stability. I also check motor condition, lubrication access, guarding, and emergency stop response. These features influence safety, uptime, and finished-part consistency. Ask suppliers for test samples, maintenance records, accuracy data, and references from comparable manufacturers. Reliable evidence is more useful than impressive claims.
A perfect choice rarely exists. I have seen buyers select oversized equipment, then face unnecessary energy costs and difficult setup procedures. Others focused on purchase price and underestimated tooling expenses. That mistake can become expensive. Consider installation space, operator training, spare parts, noise, and after-sales support before signing an order. Independent inspection may reveal issues hidden during a brief demonstration. It is worth the effort.
This guide explains how to compare a Copper Stamping Machine with greater confidence. It connects technical specifications with real production needs. The recommendations are practical, but every factory has different conditions. Verify critical information with qualified engineers, equipment manufacturers, and applicable safety authorities. Careful judgment still matters.
Identify Copper Grade and Thickness: Annealed Copper Is 100% IACS (58 MS/m)
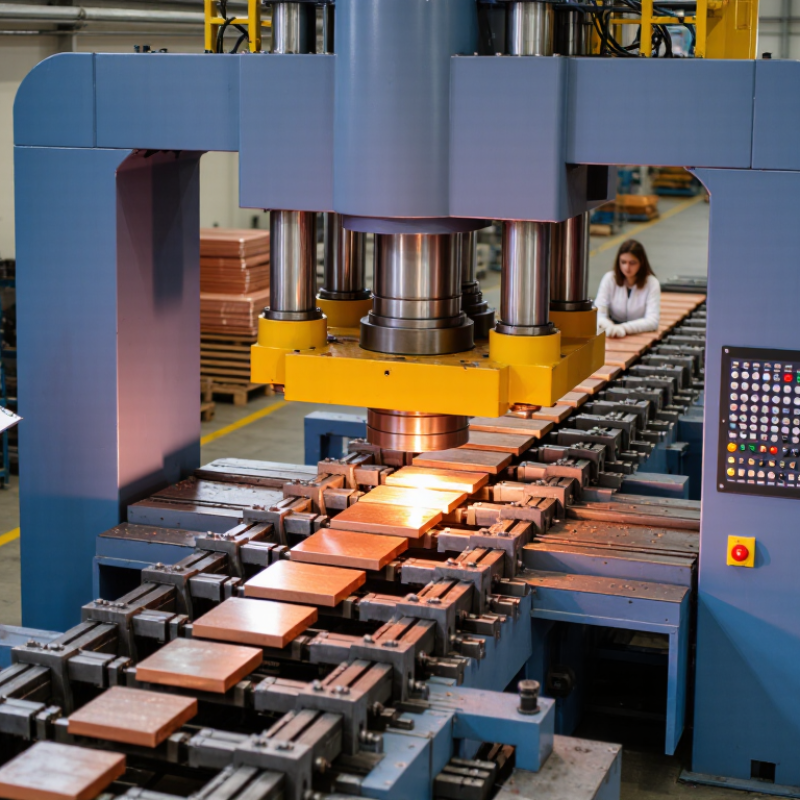
When choosing a copper stamping machine, begin with the copper grade and thickness. These properties affect force, speed, tooling, and material feeding. Annealed copper is soft and highly conductive, measuring 100% IACS, or approximately 58 MS/m. It usually needs less stamping force than harder tempers. However, its softness can increase burrs, surface marks, or deformation during feeding. A machine with stable pressure control is valuable here.
Measure the sheet with a micrometer, not only from the supplier’s specification. Thickness can vary across one coil. For example, a thin 0.5 mm sheet may require different clearance from a 1.5 mm sheet. The selected machine should provide enough tonnage without running continuously near its limit. Leave practical capacity for piercing, forming, and small material variations. I once underestimated springback in a trial. The calculation looked correct, but the finished part still needed adjustment.
Tips: Record copper conductivity, temper, width, and thickness before machine selection. Check the recommended die clearance for annealed copper. Inspect the first stamped parts under strong light. Look for burrs, edge cracking, scratches, and uneven bends. A slower trial cycle often reveals feeding problems earlier. Also review press rigidity, stroke control, and maintenance access. These details seem minor, yet they can influence repeatability more than rated tonnage.
Estimate Press Capacity with F = L × t × τ and a 20–30% Safety Margin
How to Choose a Copper Stamping Machine?
Press capacity starts with a practical estimate, not guesswork. Use F = L × t × τ, where L is the cut length, t is copper thickness, and τ is shear strength. Keep units consistent. If L is 800 mm, t is 1.5 mm, and τ is 210 N/mm², the cutting force is 252,000 N, or about 25.7 metric tons. Add a 20–30% safety margin, giving a recommended capacity of approximately 31–33 tons.
Material condition changes the result. The Copper Development Association reports that C11000 copper can reach roughly 210 MPa tensile strength, depending on temper and testing condition. Shear strength is not identical to tensile strength. ASM Handbook, Volume 14B, also emphasizes that clearance, tool geometry, and forming method affect stamping force. Therefore, treat the formula as a starting point, not an absolute specification.
Leave room for process variation. A narrow die clearance may increase force and edge damage. A progressive tool may create peak loads at different stations. I would also check the machine’s rated capacity at the actual stroke position, not only its headline rating. That detail is easy to miss. Production trials, force monitoring, and the supplier’s tooling data should confirm the final selection. An oversized press can waste energy, while an undersized press may produce unstable cuts and premature tool wear.
Select Die Clearance at 5–10% of Sheet Thickness for Burr Control
How to Choose a Copper Stamping Machine?
When choosing a copper stamping machine, start with the material grade, sheet thickness, and required production speed. Copper conducts heat quickly and can deform around the cut edge. Die clearance strongly affects burr formation, tool wear, and dimensional accuracy. A practical starting point is 5–10% of the sheet thickness. For a 1 mm copper sheet, clearance may range from 0.05 to 0.10 mm per side, depending on the tooling method. Do not treat this range as a fixed rule. Harder copper alloys, narrow features, and worn punches may require adjustment.
Observe the first production samples under magnification. A small, even rollover suggests suitable clearance, while heavy burrs may indicate excessive clearance or a dull punch. Tight clearance can produce cleaner edges, but it may increase punching force and accelerate tool damage. Machine capacity should exceed the calculated force, not merely match it. Stable guides, accurate ram alignment, and controlled lubrication also matter. In practice, operators often need several trials. The first setting may be wrong.
Tips: Record sheet thickness, alloy condition, clearance, press force, and burr height. Check the punch edge after each trial. Keep test pieces from approved settings for future comparison. If burrs appear only on one side, inspect alignment before changing clearance. That simple check can prevent unnecessary tooling changes. Converse with your toolmaker when the result remains inconsistent.
Match Stroke, Speed, and Feed Accuracy to Part Geometry and Tolerances
How to Choose a Copper Stamping Machine?
Match stroke, speed, and feed accuracy to part geometry and tolerances. Copper conducts heat quickly. The Copper Development Association reports approximately 100% IACS conductivity for annealed copper. That conductivity can increase heat transfer at the tooling interface. Choose a press with stable speed control and effective die cooling.
Stroke must clear the part without wasting cycle time. Deep drawn terminals need longer stroke and controlled forming speed. Flat clips usually need shorter motion and faster production. The International Copper Study Group reported global refined copper usage near 26 million tonnes in 2024. This growing demand makes stable throughput valuable, but speed alone is not enough. A fast machine with poor feeding can create burrs, scratches, and inconsistent hole positions.
Tips: Measure the actual coil thickness, width, and temper before selecting the feeder. Match feed accuracy to the tightest feature, not the average dimension. For high-tolerance connectors, verify repeatability under production heat. ISO 9283 performance testing can help evaluate positioning behavior, although it does not replace stamping trials. I have found that laboratory settings can look perfect. Production coils may behave differently. Leave adjustment capacity in the specification. It is easy to underestimate springback, material variation, and die wear. A practical trial should record stroke position, feed error, line speed, burr height, and part temperature.
How to Choose a Copper Stamping Machine? - Match Stroke, Speed, and Feed Accuracy to Part Geometry and Tolerances
| Part Geometry / Application | Typical Copper Alloy | Material Thickness
(mm) | Recommended Stroke
(mm) | Recommended Speed
(SPM) | Required Feed Accuracy
(mm) | Typical Part Tolerance
(mm) | Machine Selection Guidance |
| Simple flat washers and discs | Commercially pure copper or brass | 0.30–1.00 | 25–50 | 120–300 | ±0.05–0.10 | ±0.05–0.15 | A high-speed mechanical press is suitable when the strip is flat and the blanking profile is uncomplicated. Use a short stroke to reduce cycle time. |
| Small electrical terminals with one bend | Phosphor bronze or copper alloy strip | 0.20–0.80 | 25–40 | 100–250 | ±0.03–0.07 | ±0.05–0.10 | Select a press with a stable slide guide, adjustable shut height, and a servo feeder. Feed accuracy should be tighter than the most critical terminal location tolerance. |
| Progressive connector contacts with multiple bends | High-conductivity copper alloy or phosphor bronze | 0.15–0.60 | 20–35 | 150–400 | ±0.02–0.05 | ±0.03–0.08 | Use a precision high-speed press with low vibration, accurate crank motion, and closed-loop servo feeding. Keep the stroke as short as the die layout permits. |
| Deep-drawn electrical cups or sleeves | Annealed copper or ductile copper alloy | 0.50–2.00 | 60–150 | 30–100 | ±0.05–0.10 | ±0.10–0.25 | Choose a press with sufficient shut height, longer adjustable stroke, controlled drawing speed, and adequate energy at the bottom of the stroke. A slower speed helps reduce wrinkling and tearing. |
| Heat-sink fins and folded conductor parts | Copper or copper-zinc alloy | 0.50–1.50 | 40–80 | 60–180 | ±0.04–0.08 | ±0.08–0.15 | Use a press with a moderate stroke and programmable feed acceleration. Confirm that the machine can maintain consistent forming height across the production speed range. |
| Busbars with holes, slots, and multiple forming operations | High-conductivity copper | 1.00–4.00 | 50–100 | 30–100 | ±0.05–0.12 | ±0.10–0.30 | Select a higher-tonnage press with rigid tooling support and sufficient energy for piercing and bending thick strip. Verify the feed system can handle the strip width and coil mass. |
| Fine-blanked precision plates and contact components | Copper alloy, brass, or nickel-silver | 0.50–3.00 | 30–60 | 40–120 | ±0.01–0.03 | ±0.02–0.05 | Prioritize press rigidity, low deflection, precise bottom-dead-center repeatability, and a high-resolution feed system over maximum speed. |
| Long strip parts requiring tight hole-to-hole pitch | Copper alloy or brass strip | 0.30–1.20 | 25–50 | 80–220 | ±0.015–0.04 | ±0.03–0.08 | Choose servo feeding with pitch compensation, reliable pilot release, and strip straightening. Excessive stroke length can amplify timing and registration errors. |
Selection Notes: The ranges shown are practical starting points for copper strip stamping and should be verified through die trials. Required press capacity depends on material thickness, shear length, tensile strength, forming load, and the number of simultaneous operations. Feed accuracy should normally be at least 25–50% tighter than the critical part-position tolerance.
Audit ISO 13849-1 Safeguards, Energy Use, Maintenance, and Total Cost
Choosing a copper stamping machine requires more than comparing pressing force and cycle speed. In production, safety design often reveals the machine’s real quality. Ask for a documented risk assessment aligned with ISO 13849-1, including the required Performance Level for each safety function. Check guarding, interlocks, emergency stops, and two-hand controls during a live demonstration.
Do not accept certificates without validation evidence. Review safety circuit drawings, diagnostic coverage, fault response, and proof that protective devices stop hazardous motion reliably. A qualified engineer should inspect the installation, not only the sales documents. Small gaps matter. A poorly positioned light curtain can create a serious blind zone.
Energy use deserves measurement, not optimistic estimates. Request power data during stamping, idle periods, and die changes. Servo-driven systems may reduce wasted energy, but the result depends on settings, material thickness, and production volume. Maintenance access is equally practical. Look for clear lubrication points, reachable electrical cabinets, quick die alignment, and available wear parts. Record service time during a trial run.
Total cost includes tooling, electricity, operator training, spare parts, scrap, and unplanned downtime. I have seen a lower-priced machine become expensive after repeated alignment adjustments. A spreadsheet can still miss lost delivery time. Ask operators what they would change after one month of use; their answer may expose weaknesses that polished demonstrations hide. Older machines can appear reliable, yet inconsistent stroke control may increase copper deformation and inspection work.